Thank you for writing to us. One of our executive will reach back to you through your submitted medium. In case there’s an urgency, feel free to connect over WhatsApp for faster response.
Prefer calling? Dial +918048033839 (International callers) or 08048033839 (Indian callers).
EPDM Rubber Profile/ EPDM Rubber Beading used in Flat Plat Solar Water Heater Collector Panels is as per BIS No. IS12933(Part II) for Thermal Shock Test.
Size: 8 x 8 for 3mm or 4mm Glass.
Size: 8 x 12 for 3mm or 4mm Glass.
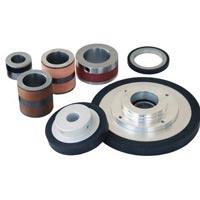
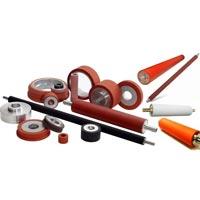
Rubber To Metal Bonded Part is a means by which rubber is mechanically bonded to a metal insert during the molding process. To begin the bonding process, the inserts are first prepped for production using a degreasing system to rid the parts of any contaminants before the adhesive is applied. Next, the heat activated adhesive is applied to the inserts using a technique similar to spray painting. Once the metals are prepared, they are ready for production.
The inserts are then physically placed, one at a time, into each cavity of the mold. For inserts on the top of a part, special magnets are incorporated into the mold to hold them in place while the mold is being loaded. Also, for inserts being encapsulated into the rubber, special chaplet pins are incorporated into the mold to suspend the insert in the mold & allow the rubber to flow around the metal.
Once the inserts are in place, the normal rubber molding process commences. After the mold is closed, and the molding begins, the adhesive on the metals is activated, allowing the inserts to bond to the rubber.
Typical applications for rubber to metal bonding include, any part requiring the combination of the flexibility of rubber and the stability of a metal. Components ranging in size from small mounts for motors to large locomotive suspension parts are just a sampling of parts produced using this process.
Rubber can be bonded with metal using more than 15 polymers including: Nitrile / Buna-N (NBR), Fluorocarbon (Viton®, Fluorocarbon (FKM), Silicone (VMQ), Fluorosilicone (FVMQ), Polyurethane (AU/EU), Natural Rubber (NR), Ethylene Propylene (EPDM), Hydrogenated Nitrile Rubber (HNBR), Styrene Butadiene Rubber (SBR), Chloroprene (Neoprene®), etc.
Silicone rubber has historically been used in specialty applications in order to meet requirements other elastomers cannot. Silicones have the largest application temperature span of all rubbers (-120 F to 500 F, with one or two exceptions where highly specialized and costly Fluoropolymers can compare).
Their chemical structure allows Silicones to be the most benign of all rubbers in medical applications (again, the exception are some very costly Fluoroelastomers). Cytotoxity tests of Silicone parts made with simple formulations show no adverse effects.
The US military applies the longest shelf life criteria to Silicone rubber components. For example, a coolant hose made with Silicone meeting SAE J20, is given a shelf life of 20 years, whereas those made with chloroprene rubber meeting SAE J20 are given a shelf life of 8 years.
The benign nature of this rubber makes components made with Silicone ideal for electronic applications, where long life and chemical inertness are essential to good electrical integrity over the component’s life. Silicone rubber parts can be made extremely conductive (resistivity of 0.0001Ω cm) or highly insulative (resistivity of 1015Ω cm).
In the automotive components market Silicone rubber has found major utilities in break line components, electrical grommets, radiator hoses, fuel line check valves (Fluorosilicone) and Oil Pan and Rocker Cover gaskets, as well as Spark Plug boots. It is estimated that in a modern car, 25% of the rubber components (excluding tires) are made of Silicone rubber
It is mostly used in Food packaging machinery, Conveyor belting industry, Electronic component manufacturing companies, PCB Panel manufacturing industry, etc.
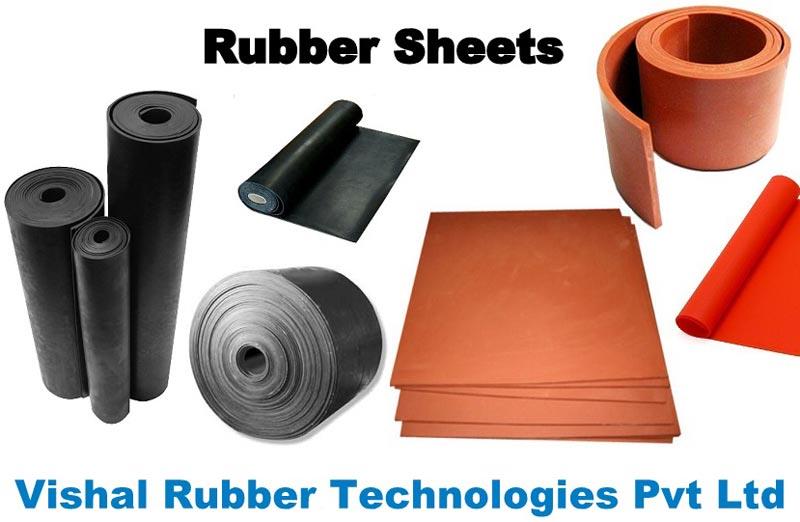
In the calendering process, fabric and rubber material is passed through a series of rollers to flatten, smooth and commingle the two or more materials. Calendered sheets can have multiple layers of both the elastomeric and polymer “sandwiched“ together.
Sheeting produced by the calender process is typically divided into two classes: either fabric inserted, or unsupported. Unsupported calender goods contain only layers of rubber or plastic that have been joined without cord, cloth or textile being inserted for strength or tear resistance. Tire cord can be used special cases; rayon, cotton, nylon, or polyester cords are arranged in parallel and bound together by rubber on a calender.
Depending upon intended use and required look or feel, the sheets of rubberized fabric are then smoothed, glazed, polished, or given a moiré or embossed surface. The resulting surface characteristics depend on the pressure exerted by the rollers, on their temperature, composition, and surface designs, and on the type of coating or glaze previously applied to the material to be calendered. Following the calendering process the material is then wound into rolls and placed into storage.
These Rubber Sheets are also manufactured from over 15 polymers including: Nitrile / Buna-N (NBR), Fluorocarbon (Viton®, Fluorocarbon (FKM), Silicone (VMQ), Fluorosilicone (FVMQ), Polyurethane (AU/EU), Natural Rubber (NR), Ethylene Propylene (EPDM), Hydrogenated Nitrile Rubber (HNBR), Styrene Butadiene Rubber (SBR), Chloroprene (Neoprene®), etc.